Contact Us

Got Questions? We're Here to Help! Contact Us.

2173 Salk Avenue, Suite 250 (#2046)
Carlsbad, CA, 92008
United States

+1 (510) 899-1340

Welcome to Service AI, your trusted source for accessories, spare parts, and certified pre-owned laboratory instrumentation tailored for scientists and startups. We provide reliable, current equipment at competitive prices, along with essential support for instruments no longer made or backed by their original manufacturers.

Our expertise spans leading brands like Beckman Coulter and Agilent, and we are committed to high-quality standards through certified maintenance, repair, and professional installation services. We believe our installation services provide the confidence and assurance you need when purchasing instrumentation from a reliable and trustworthy source.

At Service AI, we don't conduct the science—we empower scientists with reliable laboratory instrumentation and spare parts that are guaranteed to perform. We trust in scientists' expertise to determine the instrumentation they need to advance their research.

With more than 25 years of experience, our dedicated team prides itself on delivering only the highest quality products. Every instrument we offer has been thoroughly tested and certified by manufacturer-trained engineers. We ensure the functionality of our products with a Full Performance Guarantee and provide proof of performance documentation when applicable.

At Service AI, we also recognize the importance of meticulous shipping and safe delivery. Our products are handled with the utmost care to ensure they arrive in perfect condition. For those who require it, we offer professional installation services to help integrate our equipment seamlessly into your operations.

Purchase our reliable scientific laboratory equipment, and we’ll provide seamless installation service worldwide for your startup or research needs.

Advance your scientific endeavors with confidence: rely on us for recertified, trustworthy instruments at reasonable prices. It’s a smart choice made simple!

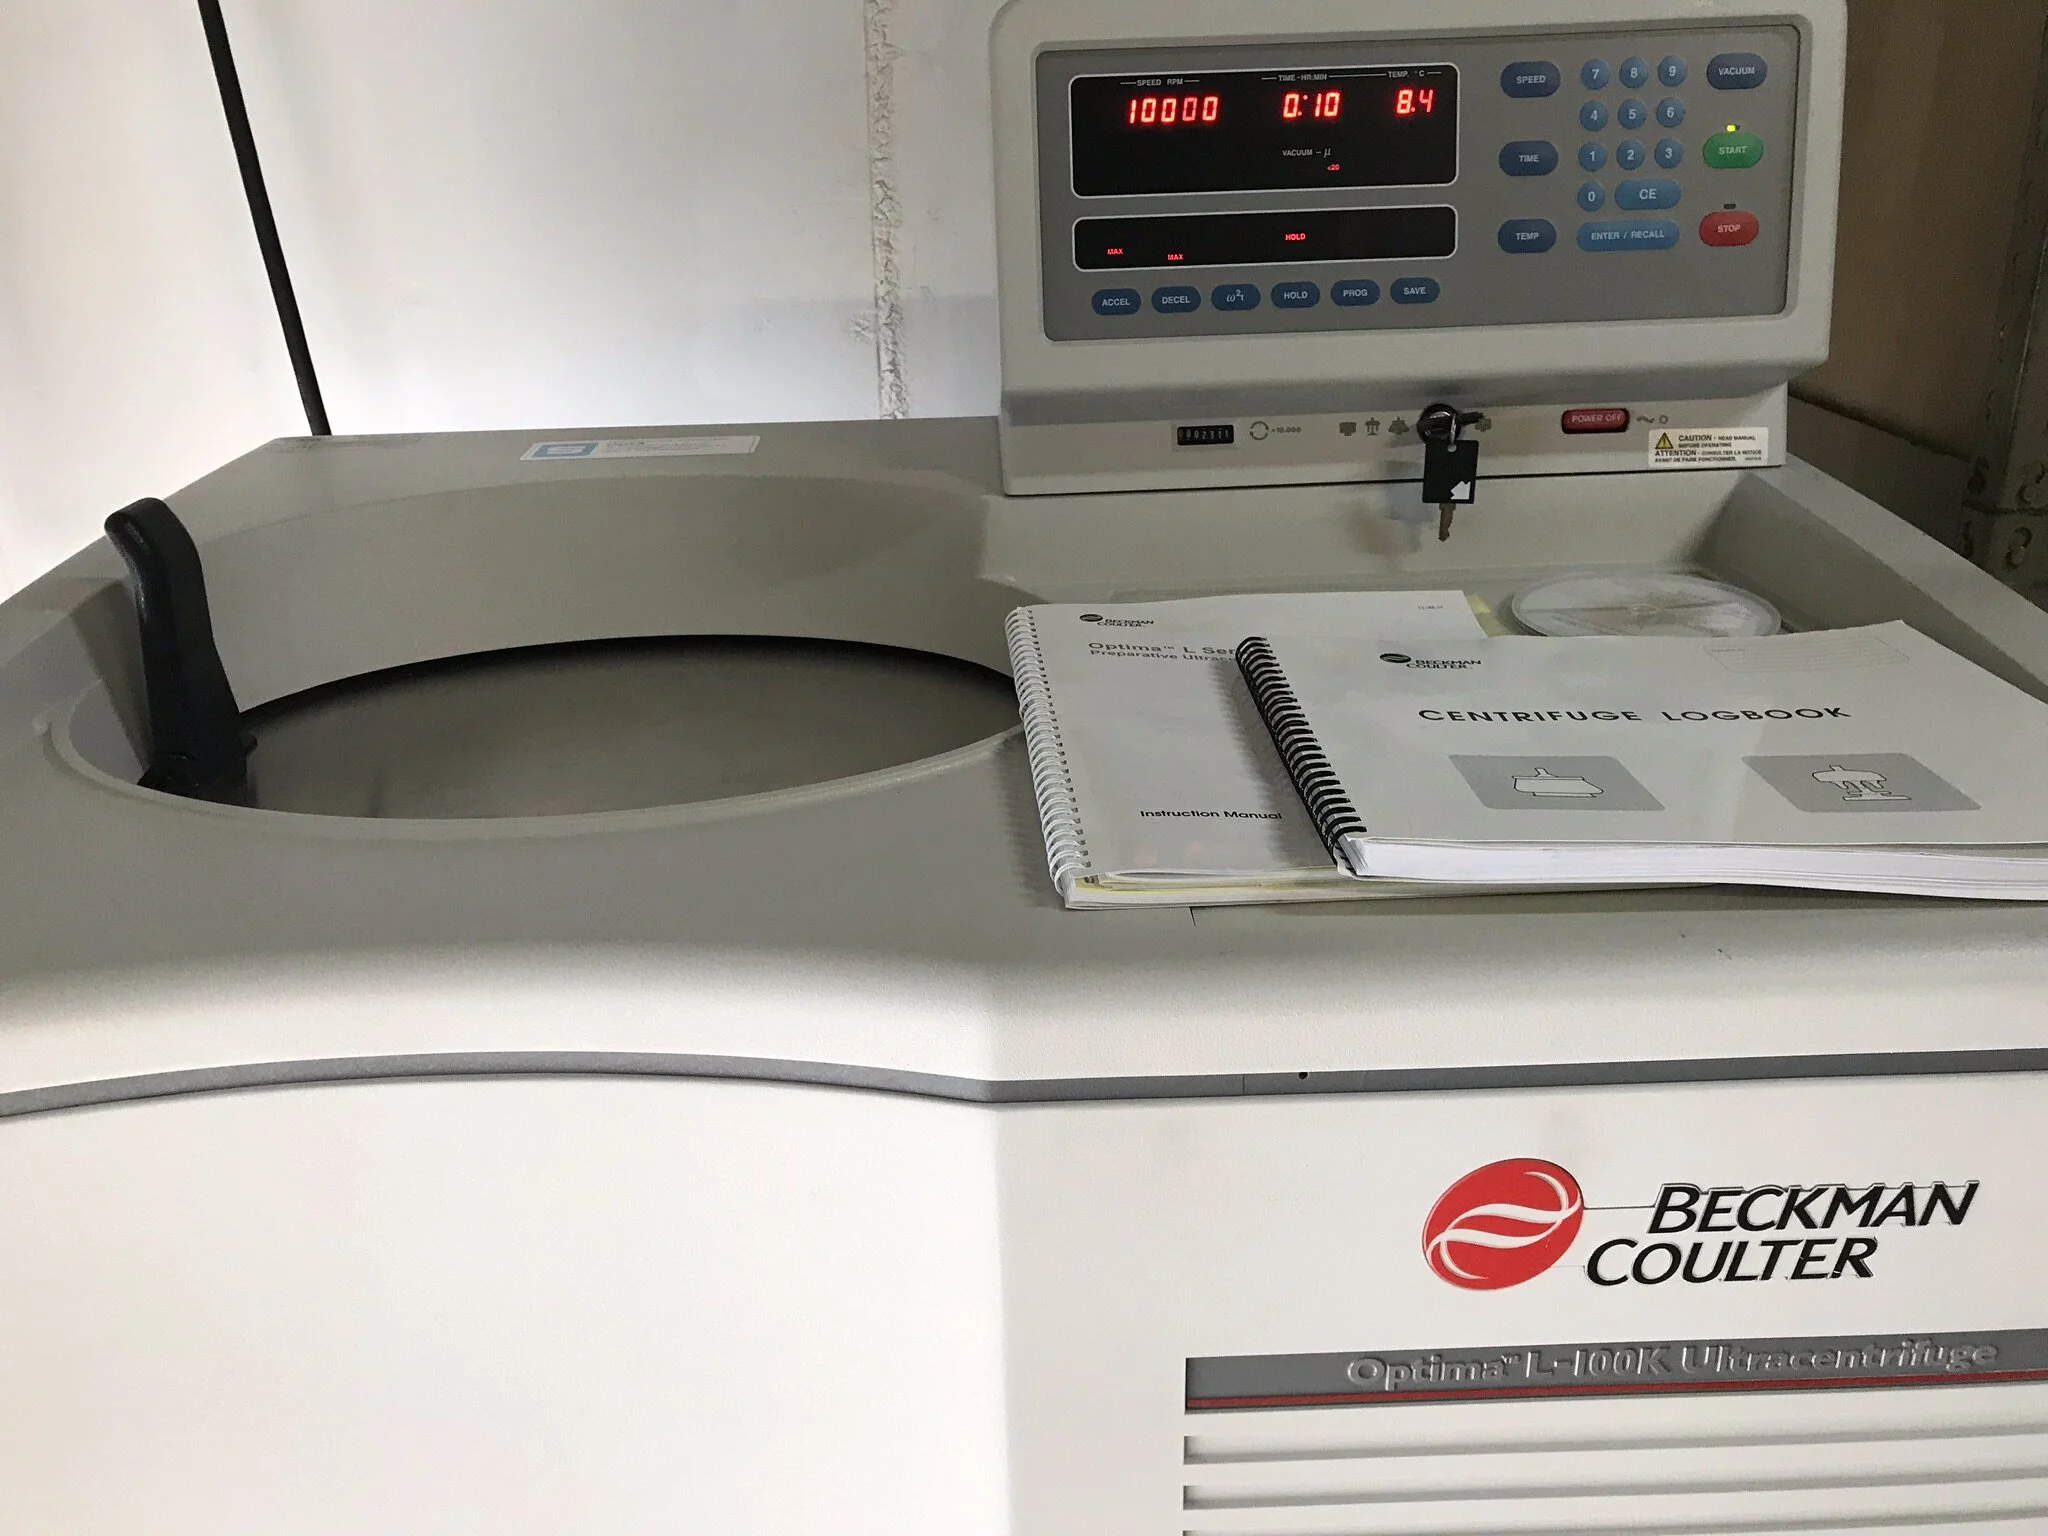
IMG_3502.JPEG

Guide to Centrifuges

Service AI support guide for centrifuge questions. Please feel free to email us at support@serviceai.us

Filtering by Tag: Beckman Optima ultracentrifuge

The Complete Guide to Centrifuge Rotor Care, Inspection, and Retirement

Service AI

From rotor design to daily care — what every lab scientist needs to know to protect their equipment, their samples, and their team.

How Much Engineering Goes Into Your Rotor?

Before diving into care and inspection, it helps to understand what you’re working with. Beckman Coulter has been at the forefront of ultracentrifuge rotor manufacturing since 1956 — a seven-decade track record that few instrument manufacturers in any field can match. The engineering behind every Beckman Coulter rotor is extraordinary. Early ultracentrifuges ran at 40,000 rpm, generating forces of around 100,000 × g. Today’s Optima XPN reaches 100,000 rpm with forces up to 802,000 × g, which means a single ounce of material in a high-speed rotor effectively “weighs” about 32 tons. That leap in performance, sustained safely over decades of continuous innovation, is a testament to how seriously Beckman Coulter takes the science of centrifugation.

Getting from blank metal to a finished rotor is a rigorous, multi-stage process:

  1. Market need and feasibility study — Engineering teams identify what researchers need and determine whether a new design is viable.

  2. Design and computer modeling — Engineers use finite element analysis (FEA) to model the stresses on every part of the rotor geometry before a single prototype is cut. Stress contour maps highlight high-risk areas so the design can be revised on screen rather than on the test stand.

  3. Material testing — Metallurgists generate stress-strain curves for candidate alloys. Notably, ultracentrifuge rotors are stressed to levels higher than jet engine components — and some designs deliberately operate beyond the yield point of the material.

  4. Prototype fabrication and safety testing — Prototypes are spun in specially modified instruments inside reinforced enclosures, operated remotely for engineer safety.

  5. Non-destructive testing (NDT) — Both prototype and production rotors are inspected using ultrasonic and dye penetrant methods to catch internal and surface defects invisible to the naked eye.

  6. Applications lab verification — Scientists run actual separations with the prototype to confirm it achieves its designed performance.

  7. Production and balance testing — Every finished rotor is spin-tested to at least its rated speed and balance-checked before receiving its protective coating.

Few instrument manufacturers subject their products to this level of scrutiny before they ever reach a customer’s lab. It is one of the reasons Beckman Coulter rotors have earned the trust of researchers across life sciences, biopharma, and clinical diagnostics worldwide. Understanding this background matters for one simple reason: a rotor represents a significant investment of engineering, material, and money — and how you handle it in the lab determines how long that investment lasts.

Why Rotor Inspection Matters: The Cost of a Failure

Rotor failures are rare, but their consequences are severe. A single failure can mean:

  • Costly instrument repairs — chamber damage, drive damage, and contamination cleanup.

  • Loss of irreplaceable research samples — sometimes representing months of collection and preparation.

  • Safety risk to laboratory personnel — Beckman Coulter ultracentrifuges are engineered with industry-leading containment systems designed to handle very high levels of rotational energy, but that containment is a last resort, not a routine safeguard. The best safety feature is a well-maintained rotor.

Rotor failures almost always have a precursor — a defect that could have been detected and addressed before it became a catastrophic event. This is why periodic rotor inspection, combined with disciplined day-to-day care, is the single most effective way to protect your lab.

Understanding Rotor Materials: Aluminum vs. Titanium

The two primary materials for centrifuge rotors are aluminum alloy and titanium alloy. Beckman Coulter has refined the use of both over decades, developing alloy specifications and manufacturing processes that push these materials closer to their theoretical performance limits than almost any other application in precision engineering. Each has distinct advantages:

Property Aluminum Titanium
Density ~0.10 lb/in³ (2.77 g/cc) ~0.16 lb/in³ (4.43 g/cc)
Corrosion resistance Lower — requires anodizing Higher — naturally resistant
Cost Lower Significantly higher
Typical service life 10 years 12 years

Aluminum remains in widespread use because its lower density means a rotor of given volume weighs less, which reduces the stress the rotor imposes on itself during high-speed operation. This weight advantage allows aluminum rotors to be built with larger capacity at a given speed. The trade-off is that aluminum is more susceptible to corrosion — which is why aluminum rotors are anodized.

Anodizing creates a thin oxide layer (approximately 0.0006 inches thick) on the aluminum surface that provides corrosion resistance — not corrosion immunity. The anodizing is deliberately kept thin because a thicker layer would become brittle and crack, which would be counterproductive. Once the anodize layer is breached by chemical attack or mechanical damage, the bare aluminum beneath is vulnerable.

Titanium has superior corrosion resistance and better strength-to-weight ratio at high stress levels, making it the material of choice for the highest-speed rotors and for labs where corrosive conditions are unavoidable. The tradeoff is cost — titanium rotors and buckets are significantly more expensive than their aluminum counterparts.

Stress Corrosion: The Primary Cause of Aluminum Rotor Failure

The number-one cause of aluminum rotor failure is stress corrosion — a synergistic combination of tensile stress and a corrosive chemical environment that produces cracking far more rapidly than either factor alone. In a rotor spinning at speed, tube holes and other geometrical features generate tensile stresses in the surrounding metal. If corrosive agents (certain buffer salts, detergents, strong acids or bases, or aggressive cleaning agents) are present, even trace contamination can initiate and propagate a crack in those stressed regions.

Stress corrosion damage is typically dark in appearance and often appears near or around tube cavities. Catching this damage early — before it propagates — is the goal of any good rotor inspection routine.

Rotor Care and Handling: Best Practices

Day-to-day care has the greatest influence on rotor lifespan. The following practices protect your investment:

Cleaning

  • Clean rotors promptly after each use. Residual samples — especially biological materials, salt solutions, and acidic or basic buffers — accelerate corrosion if left in contact with the rotor surface.

  • Use only manufacturer-approved cleaning solutions. These are formulated to clean effectively without attacking the anodize layer or rotor alloy, and some provide an additional protective benefit to the rotor surface.

  • Rinse thoroughly and dry completely before storage. Moisture trapped in tube holes or under O-rings is a common initiator of corrosion.

  • Do not heat aluminum rotors above the manufacturer-specified maximum temperature. Elevated temperatures alter the metallurgical properties of the alloy and can compromise the integrity of the anodize layer.

Storage

  • Store rotors inverted or as directed in the rotor operator’s manual to prevent moisture accumulation in tube holes.

  • Store in a clean, dry environment away from corrosive fumes (ammonia, acids, solvents).

  • Never store rotors with sample tubes in place.

Tube Caps and O-rings

  • Inspect tube caps and O-rings before every use. Replace caps showing wear, cracking, or deformation — do not attempt to reuse damaged caps.

  • Ensure sealing surfaces are clean and dry before assembling. Wet O-rings can wick fluid outward during a run, causing a leak and potentially contaminating the rotor cavity.

Rotor-Centrifuge Compatibility

  • Always run rotors only in compatible centrifuges. Each rotor is designed, tested, and rated for use with specific instruments. Running a rotor in an incompatible centrifuge introduces safety risks and may invalidate any remaining warranty.

  • High-energy rotors have built-in design features that limit the maximum speed they can reach in a runaway event. These features only function correctly in compatible instruments.

Special Considerations for Swinging-Bucket Yoke Rotors

  • Yoke-style swinging-bucket rotors require special care during cleaning, particularly around hinge pins and yoke pivot points. Always follow the specific cleaning procedures in the rotor operator’s manual — these are critical structural components.

Rotor Service Life and Retirement — Know the Numbers

Rotors are not lifetime consumables. They have defined service life limits based on engineering analysis of fatigue accumulation. It is worth noting that Beckman Coulter’s retirement guidelines are deliberately conservative — they are designed to ensure safety well before a rotor approaches the outer edge of its theoretical fatigue life, which reflects a commendable commitment to lab safety over commercial considerations. The figures below reflect general industry guidance for Beckman Coulter preparative rotors; always verify current specifications against your rotor’s operator manual or by contacting a qualified service provider, as these figures can be updated by the manufacturer.

Ultracentrifuge Rotors

Rotor Type Typical Warranty (Years) General Retirement Guideline (Years)
Swinging Bucket 5 10
Aluminum Fixed Angle 5 10
Titanium Fixed Angle / VT / NVT 5 12
Composite Rotors 5 12
Analytical Aluminum 5 10
Analytical Titanium 5 12
TL Series 5 12
Airfuge Rotors 1 10
Zonal & Continuous Flow 5 10

Avanti J-Series Rotors

Rotor Type Typical Warranty (Years) General Retirement Guideline (Years)
Avanti J Series 7 15
J 2/6 Series 7 15
JLA-10.500 Canister 7 7

Note: Some canisters have a retirement date engraved directly on them. Always check before use.

Benchtop Rotors

Rotor Type Typical Warranty (Years) General Retirement Guideline (Years)
Standard Benchtop Rotors 7 10
Allegra X12 Series 1 5
Benchtop Plastic Rotors 1 5

Why Retirement Limits Matter Even for Rotors That Look Fine

Many researchers assume a rotor that looks fine is fine. The reality is that metal fatigue accumulates invisibly. Rotors that operate at high stress levels experience incremental microcracking with each run — damage that cannot be detected by appearance alone. A rotor showing no visible defects at year 12 has still accumulated fatigue that makes continued operation a risk. Always retire rotors according to the limits specified in the operator manual, regardless of outward condition.

A rotor should also be considered for speed deration if:

  • It has sustained tube cap land damage.

  • It shows evidence of corrosion that has been cleaned but not fully repaired.

  • It has been operated outside its specified temperature range.

If you’re unsure whether a rotor should be derated or retired, contact the Service AI team for guidance — our factory-trained engineers can help you assess the situation.

When to Have a Rotor Professionally Inspected or Assessed

Some rotor conditions go beyond what visual checks in the lab can resolve. Seek professional evaluation when:

  • You notice any discoloration, pitting, unusual surface texture, or dark areas near tube cavities — these can be early signs of stress corrosion.

  • A rotor has been involved in an incident — an imbalance event, suspected over-speed, or a chemical spill into the centrifuge chamber.

  • A rotor is approaching or has reached its retirement age or run-count limit and you need a qualified assessment before making a retire-or-continue decision.

  • Tube cap lands show damage or deformation, and you’re uncertain whether deration is sufficient.

Service AI’s factory-trained engineers are available to assess rotors, advise on care and handling, and help you source certified replacement rotors or compatible spare parts when retirement is the right call. Keeping your lab running safely is what we do.

Summary: The Lab Scientist’s Rotor Checklist

  • ✅ Clean and dry rotors after every use

  • ✅ Use only manufacturer-approved cleaning solutions

  • ✅ Inspect tube caps and O-rings before every run

  • ✅ Log run counts and dates — know where your rotor stands against retirement limits

  • ✅ Schedule periodic professional rotor inspections, especially for rotors approaching 5+ years of age

  • ✅ Only run rotors in compatible centrifuges

  • ✅ Retire rotors that have reached their age or run-count limit, regardless of appearance

  • ✅ Contact a qualified expert any time you’re uncertain about a rotor’s condition

Your centrifuge rotor is one of the most highly engineered components in your laboratory. Treat it accordingly.

Have questions about rotor condition, sourcing a replacement, or finding compatible spare parts? The Service AI team is here to help. Reach us at support@serviceai.us or call +1 (510) 899-1340.

Visit serviceai.us for our full inventory of recertified Beckman Coulter and Agilent laboratory instrumentation.

Essential Guide to Centrifugation Labware: Tubes and Bottles

Service AI

Centrifugation is a fundamental technique in biological and bioindustrial research, and the choice of labware—tubes and bottles—plays a crucial role in the efficiency and success of this process. This guide covers key aspects of centrifugation labware, including material selection, design considerations, chemical resistance, and maintenance.

Read More

Introduction to Centrifugation

Service AI

Centrifugation is a technique used to separate particles in a solution by applying a centrifugal force. In biological research, these particles often include cell organelles or large molecules.

Read More

Troubleshooting Vacuum Issues in Beckman Coulter Ultracentrifuges: A Comprehensive Guide

Service AI

In an ultracentrifuge, it is crucial to remove air molecules from the 'leak-tight' chamber. To achieve this, Beckman uses a mechanical vacuum pump and diffusion pump in combination. However, in high-performance and high-speed model centrifuges, only a vacuum pump is necessary.

Mechanical vacuum pumps, also known as roughing pumps or forepumps, are the only types that can operate against atmospheric backpressure. The most commonly used mechanical pump is the vane type.

The actual removal of air molecules occurs during four stages of the pumping cycle: intake, transfer, compression, and exhaust.

Vacuum system in an ultracentrifuge

Beckman Coulter ultracentrifuges use vacuum pumps that are characterized by the following features:

 • Two-stage, oil-sealed, rotary vane type

• Maximum vacuum of 20 microns at the inlet

• Pump speed of around 7 cubic feet per minute (cfm)

• Direct drive design with motor in-line with the pump

• Anti-suckback system included

• Mechanical oil stirrer system

• Gas ballast to allow pumping of condensable vapors

• Inlet, outlet, and muffler connections

• Sight glass to indicate oil level

• Easy disassembly into major parts for cleaning and repair

• Motors that can be wired for different voltage requirements

Beckman Coulter ultracentrifuge systems utilize a combination of a diffusion pump and a vacuum pump in series to achieve high levels of vacuum. However, the diffusion pump alone is not capable of exhausting to the atmosphere. As a result, it is exclusively employed in the ultracentrifuge models.

As shown in the diagram below, the Diffusion Pump Assembly consists of the following parts:

• Pump body: a steel cylinder with an oil reservoir at the base of the pump

• External cooling jacket or fan assembly attached to the pump body

• Jet assembly: a hollow assembly with nozzle(s)

• Cold Cap assembly attached to the inlet

• Inlet and exhaust outlet

• Electrical heater assembly

• Low vapor pressure oil (Use only the Beckman Coulter recommended silicone diffusion pump oil.)

Schematic of a diffusion pump

During normal operation of a Beckman Coulter ultracentrifuge, the vacuum pump runs first. The diffusion pump fan assembly operates. The oil reservoir heater is activated depending on the vacuum level, heating the oil until it boils. The hot oil vapor is then released through the jet nozzles, expanding as it moves from high to low pressure. As gas molecules (air and water) enter the diffusion pump inlet, they collide with the heavy oil vapor stream and are directed towards the pump's exhaust outlet by the vacuum pump. The supersonic vapor jet of diffusion pump oil then strikes the cooled diffusion pump wall, causing the oil vapor to condense and flow back into the oil reservoir to begin the cycle anew.

To achieve the necessary vacuum conditions in ultracentrifuges, the diffusion pump must be used in series with a vacuum pump. The diffusion pump cannot be exposed to the atmosphere while the oil is hot due to potential oil degradation and vacuum system contamination.

The lowest pressure achievable in the ultracentrifuge vacuum systems is partly limited by the presence of oil vapor from the diffusion pump. This occurs due to "backstreaming" of oil vapor molecules from the diffusion pump nozzle towards the inlet, as well as "back migration" caused by re-evaporation of oil at the top of the pump body.

The amount of backstreaming can be reduced by optimizing the pump nozzle design and using cold caps, traps, or baffles above the pump body. Controlling the temperature of the pump housing and the baffle system can also reduce back migration.

While this backstreaming and back migration is not a significant issue for typical preparative ultracentrifuges, the oil vapor can be problematic for the optical systems of analytical ultracentrifuges.

The diffusion pump is a low-maintenance component, with no mechanical moving parts. However, it is important to perform regular maintenance to ensure optimal performance. Here are the recommended maintenance tasks:

Check the diffusion pump oil regularly and change it if it appears light to dark brown in color.

  1. Remove the jet assembly once a year for inspection and cleaning.

  2. Inspect the oil heater and check its resistance.

  3. Inspect and clean the cooling fan and verify its operation.

Here are some troubleshooting tips for the diffusion pump: 

Oil Heater Assembly - If the heater is burned out, the system will only achieve a normal mechanical pump vacuum level (less than 100 microns). The reason for heater failure may be due to loss of oil, hours of operation, or loss of cooling.

Loss of Fluid - Normally, loss of fluid is due to a leak in the vacuum system.

Cooling Fan Malfunction - This causes a loss of diffusion pump cylinder cooling.

Loss of Vacuum - The system will initially achieve the correct vacuum. As the pump cylinder heats up, the vapor no longer condenses, and loss of vacuum occurs.

Diffusion Pump Fluid Contamination - If the drive oil or liquid from the rotor spills into the diffusion pump, it may cause the pump to lose effectiveness.

PMC Check - Check for the correct oil level, heater function, and air flow.

Normal Loss of Vacuum - With a chamber vacuum of 150 microns or better, it is normal to see a slight loss of vacuum immediately after turning on the diffusion pump heater.

Vacuum System Troubleshooting: Finding and Fixing Leaks:

  1. Check for obvious issues such as cracked hoses, tubing, and foreign material on "o" rings.

  2. Confirm the mechanical pump is working properly by measuring the vacuum level at the pump inlet, which should be less than 20 microns. Replace vacuum pump oil on a regular basis.

  3. Be aware that removing moisture from a vacuum system can take time, and during this period the vacuum level will remain at approximately 500 microns.

  4. For larger leaks, turn off power and listen for a hissing sound to detect the source of the leak.

  5. Try to isolate sections of the vacuum system to narrow down potential leak locations.

  6. Use acetone to identify leaks: if you're able to obtain a vacuum of 300 microns or less, squirt acetone on possible leak areas. The vacuum indicator will exhibit a loss of vacuum at the area where the leak is present.

  7. Ensure the diffusion pump is functional by following proper maintenance and troubleshooting procedures.

How to Change Vacuum Pump Oil in Beckman Optima and Avanti J30I Centrifuges

Service AI

Prior to draining the oil, it is always best to operate the vacuum pump until it is at its normal operating temperature of approximately 65ºC.

  •  Always take a test run in the ultracentrifuge with the vacuum pump running to warm up the existing oil. When the pump oil is warm it is less viscous and contaminants will mix with the oil.

  •  Stop the test run. Release vacuum by depressing the "VACUUM" key on the ultracentrifuge keypad, which will stop the vacuum pump and release the vacuum. Turn off power to the instrument and unplug the instrument power cable from the AC Mains.

  •  Disconnect the vacuum pump power cord. Disconnect the vacuum hose from the inlet port. Remove the vacuum pump from the centrifuge. Place the vacuum pump on the flat surface to perform the work.

  • Remove the exhaust filter. Locate the vacuum pump drain plug. Place the waste oil container under the drain plug. Remove the drain plug. Drain the oil. Always consider and treat the waste oil as hazardous. Hand over the waste oil container to the laboratory safety official at the site for disposal.

  •  Replace the drain plug.

  •  Remove the oil fill plug (normally on top of the pump housing) Add Vacuum pump oil until the correct level is reached in the sight-glass. Replace the oil fill plug.

  •  Replace the exhaust filter. It is good practice to always install a new exhaust filter after oil replacement as a part of the preventive maintenance procedure.

  •  Replace the vacuum pump into the centrifuge. Inspect the vacuum pump hose carefully before reconnecting it to the vacuum pump. Replace hose if you observe faults or fine cracks in it.

  •  Reconnect the power cord. Make a test run to verify proper operation of the vacuum pump and centrifuge.

 Important tips:

  •  Do not mix hydrocarbon based oils with synthetic oil in vacuum pumps.

  •  Use only “Beckman” Direct Drive Vacuum Pump Oil (Beckman PN. 341661 and Beckman PN. 392760) or oil that is recommended by vacuum pump manufacturer.

Optima ultracentrifuge flags persistent Diagnostic d63 Drive error

Service AI

If your Beckman Coulter Optima ultracentrifuge flags d63; it is an indication that the drive thermostat mounted on the drive has overheated (causing an open circuit) during normal run, or that it did not cool down and get deactivated after a 5 minute waiting period on power up. When a power fail diagnostic occurs during a normal run, the ultracentrifuge will shut down with brake.

If this fault occurs, a Beckman trained and experienced expert will make it a point to check the drive, drive oil, drive fans,  and the drive control system of the ultracentrifuge.

website: www.serviceai.us ; email: support@serviceai.us; Technical Support: +1-510-899-1340

How to Install a Beckman Coulter Optima Ultracentrifuge

Service AI

Important Note: To ensure proper electrical installation and checkup as outlined below, it is imperative to engage a certified electrician for power requirements. Furthermore, we highly recommend that a qualified engineer handles the installation and thorough inspection of your Beckman Coulter Optima L ultracentrifuge, while also providing training to your staff on its correct usage and handling of the ultracentrifuge and rotors before operation.

Power:

a. Check for correct wall receptacle and voltage at the outlet. Power required is 180 to 264 Volts AC measured as shown. It is advisable to test the line voltage at the plug while the instrument is accelerating and cooling; therefore, we would strictly recommend that the ultracentrifuge always be installed by a Beckman trained engineer. Service AI has Beckman Coulter trained service experts. You can email us at support@serviceai.us, or call us at our technical support line at +1-510-899-1340 for more information.

b. Remove console cover, front panel and top cover.

c. Make sure jumper connector on the power supply boards plugged into the correct voltage range socket J52 A, B, or C. (Select the jumper for the lowest voltage reading during maximum power consumption.)

J52 VOLTAGE RANGE

A 180 - 206

B 207 - 233

C 234- 264


Physical installation procedure:

a. Position ultracentrifuge in desired location. Maintain 6" minimum clearance at rear and 3" minimum clearance at each side.

b. Position the four pads provided under the leveling legs. Mark the position of each pad on the floor.

c. Roll out instrument away from pads.

d. Glue (epoxy) pads to floor.

e. Roll instrument back into position and screw the four leveling legs down into the pads until they have bottomed out.

f. Now screw each leveling leg down five additional turns. Make sure all four casters are off the floor.

NOTE: A solenoid inter-lock prevents the chamber door from being opened during operation and/or with the power off. The chamber door can be opened with the door handle only when the power to the ultracentrifuge is on and the vacuum is off.

g. Open the chamber door (see note above). Level the ultracentrifuge as if it had only three legs. Adjust level by placing the spirit level on the drive shaft (crown) and adjust the leveling legs so the air bubble is centered. First level it front- to- rear by adjusting the left front and left rear legs. Then level it left to right by adjusting the right front leg only. (Make sure you do not tilt the instrument). Screw in the right rear leg until it just touches the pad. Now screw it down 1/4 turn more. This does not affect the level of the instrument.

spirit level.jpg


h. After instrument is leveled, make sure all four casters are off the floor and all four leveling legs are still bottomed out.


website: www.serviceai.us; email: support@serviceai.us; technical support: +1-510-899-1340

Official   PayPal Seal